Component mispicks and gradual feeder drift remain the primary sources of placement yield loss on compact Surface Mount Technology (SMT) assembly lines.
Operators running the 4-head CHM-551 pick-and-place system often trace intermittent empty-nozzle cycles, skewed passive chips, and false vision rejections back to minor mechanical or pneumatic variances rather than controller faults.
Stabilizing placement repeatability requires aligning compressed air delivery, Z-axis touchdown depth, and upward optical thresholds with SMT process validation practices and the IPC-9850 placement standard
Root Causes of Feeder Drift and Mispicks on the CHM-551
Mechanical play and air-supply fluctuations compound quickly across high-speed multi-head placement cycles. Identifying which subsystem introduces variance prevents operators from masking hardware drift with temporary software offsets.
Pneumatic Pressure Fluctuations in Yamaha CL Feeders
Standard Yamaha CL pneumatic feeders mounted across the CHM-551’s 50-slot carriage depend on steady compressed air between 0.5 MPa and 0.7 MPa (72 to 100 PSI) to actuate their indexing cylinders. When facility air lines drop in pressure during simultaneous multi-nozzle cycles, the feeder pawl fails to complete a full advance stroke.
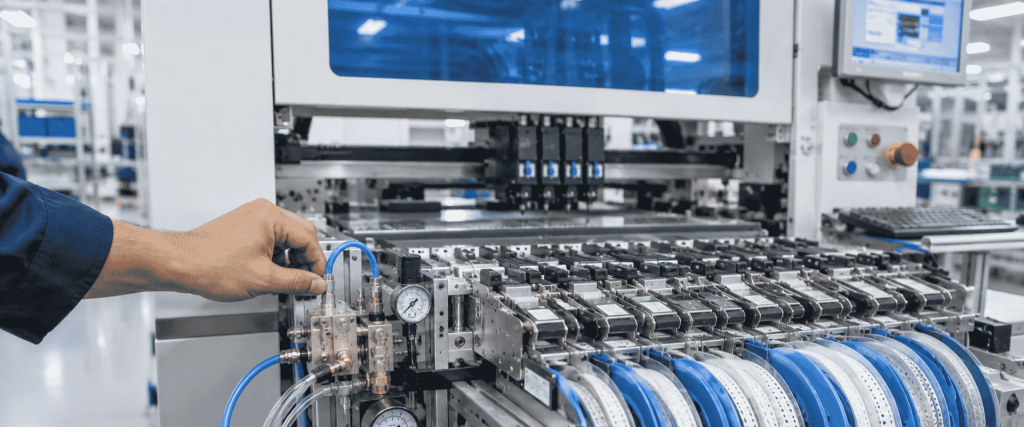
Half-pitch tape advancement leaves the component pocket offset by 1-2 mm, causing the nozzle tip to strike the carrier tape edge instead of the component center. Maintaining cleanroom metrology standards for dry, regulated pneumatic lines prevents moisture buildup and sluggish cylinder return inside older feeder bodies.
Mechanical Wear and Tape Pitch Misalignment
Repeated reel changes and worn ratchet pawls introduce progressive lateral drift over multi-hour production runs. Common mechanical contributors include:
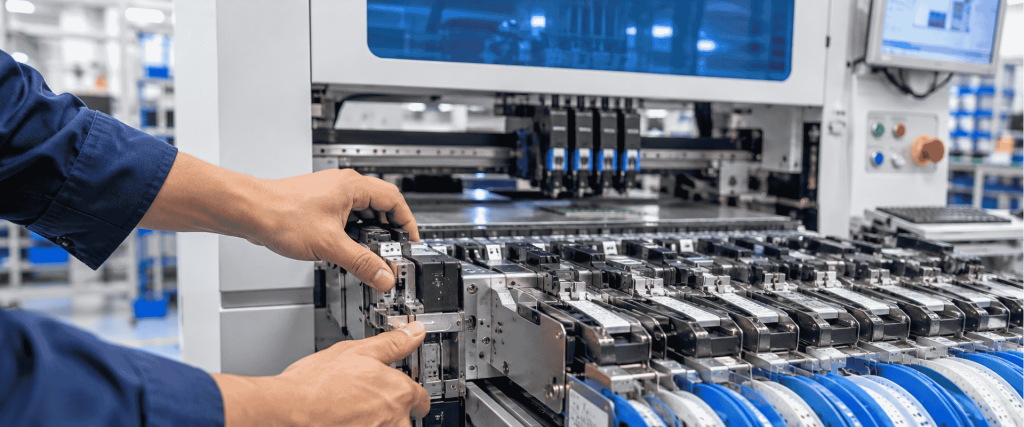
- Unlatched Feeder Bases: A feeder body that is not fully seated against the CHM-551 mounting rail tilts slightly upward, shifting the X-Y pick point by up to 0.3 mm.
- Incorrect Pitch Selector Settings: Running 0402 components on a 4 mm feed setting instead of a 2 mm pitch skips every second pocket and triggers consecutive empty-pick alarms.
- Loose Cover-Tape Take-Up Reels: Slack peel-back tension allows clear carrier film to hang over the exposed pocket, blocking nozzle suction.
Nozzle Vacuum Decay and Z-Axis Touchdown Variance
Micro-nozzles designed for 0201 and 0402 passives rely on unobstructed internal bores and intact rubber O-rings to maintain negative pressure during rapid X-Y gantry acceleration. Flux residue, paper tape fibers, or microscopic solder spheres restrict airflow and lower vacuum sensor readings below the controller’s detection threshold.
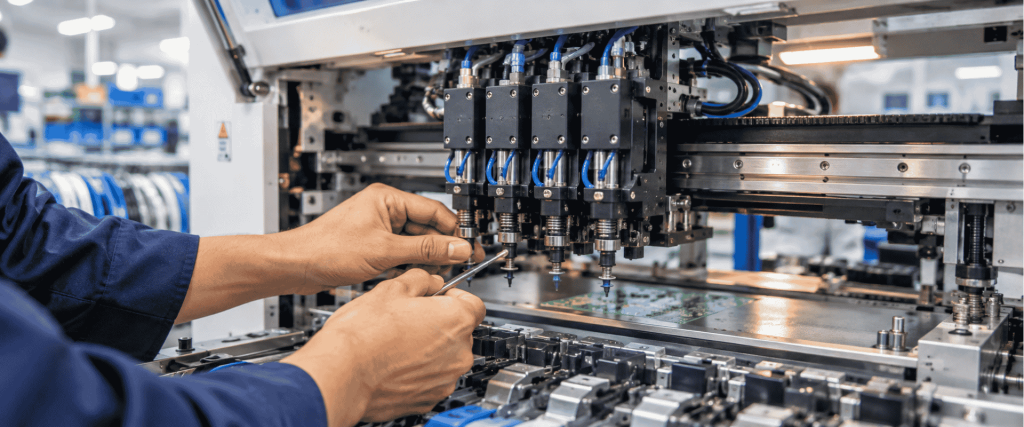
Reference tolerances aligned with NIST metrology traceability demonstrate that even a 0.15 mm error in Z-axis pick height either fails to compress the nozzle spring enough to create an airtight seal or crushes thin ceramic capacitors against the bottom of the carrier pocket.
Step-by-Step Calibration to Eliminate Placement Errors
Systematic calibration isolates mechanical positioning from optical compensation so each of the four placement heads picks and places within its specified tolerance.
Regulating Air Supply and Indexing Feeder Pick Coordinates
- Install a Dedicated Point-of-Use Regulator: Set a precision air regulator and coalescing filter directly at the CHM-551 manifold to hold a constant 0.58 MPa (84 PSI) under full four-head load.
- Seat and Lock Each Feeder Stack: Press every feeder firmly forward until the locking pin engages the rail slot, then verify zero vertical play by hand.
- Teach Pick Centers Optically: Use the downward-facing mark camera to capture the exact geometric center of an exposed component pocket rather than relying on theoretical slot grid coordinates.
- Verify Five Consecutive Advance Cycles: Trigger five manual feed pulses on each active slot and confirm the component stays centered beneath the downward camera crosshair.
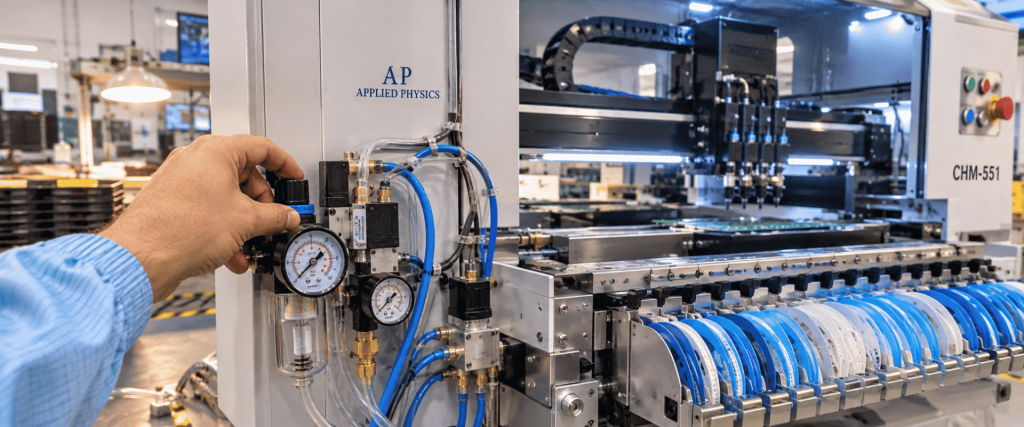
Follow structured equipment qualification protocols whenever swapping feeder banks between product changeovers to lock in repeatable X-Y pick coordinates.
Calibrating Z-Axis Pick Heights and Vacuum Thresholds
- Zero the Nozzle Tip Against the Carrier Pocket: Lower each nozzle slowly in manual step mode until the tip contacts the top surface of the component, then add 0.15 mm of spring buffer travel.
- Measure Baseline Vacuum Values: Record the open-air vacuum reading and the loaded-component vacuum reading for each head inside the controller diagnostics screen.
- Set Midpoint Detection Thresholds: Configure the vacuum alarm threshold midway between the open-air and loaded values so missing or tilted parts trigger an immediate re-pick before gantry transit.
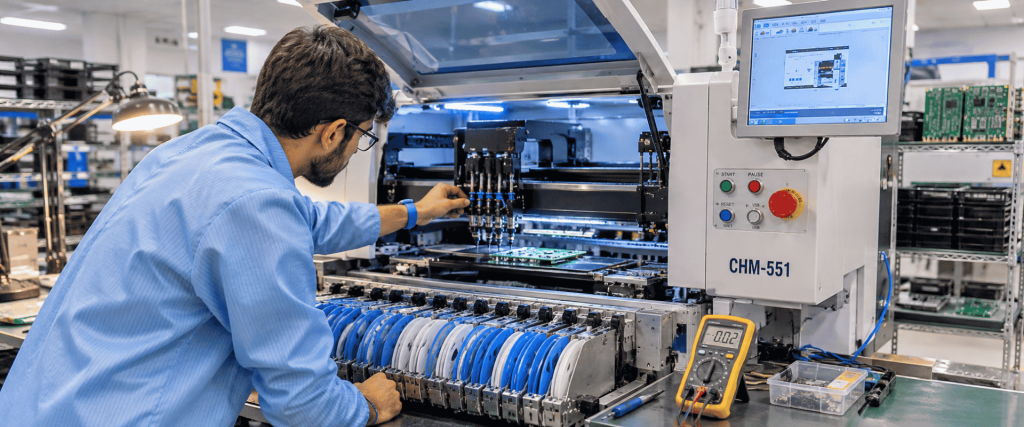
Tuning Upward Vision Lighting for Reflective Packages
Specular reflections from tinned QFN leadframes, metallic RF shields, and glass-bodied diodes frequently confuse standard upward CCD camera thresholds.
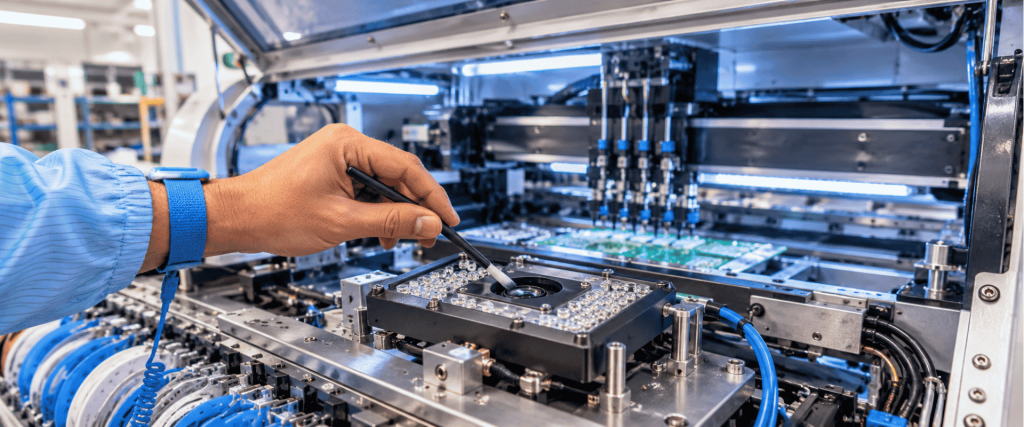
Lowering the primary ring-LED intensity while increasing camera exposure time eliminates bright hotspots that obscure true package edges. Cross-checking lead geometry against JEDEC packaging standards ensures the vision algorithm measures true outer pin boundaries rather than false glare halos.
CHM-551 Diagnostic Matrix and Corrective Parameters
Operators can use the diagnostic matrix below alongside semiconductor inspection guides to isolate recurring placement faults during live production runs.
| Symptom / Failure Mode | Primary Root Cause | CHM-551 Verification Check | Corrective Action & Target Spec |
| Intermittent empty-nozzle mispicks on 0201/0402 reels | Restricted nozzle bore or insufficient Z-axis spring compression | Compare open-air vs. loaded vacuum pressure in diagnostics | Clean nozzle bore ultrasonically; set Z-axis touchdown buffer to 0.15 mm |
| Progressive lateral drift across consecutive picks | Pneumatic feeder pressure drop or worn ratchet pawl | Cycle feeder 10 times under downward camera crosshair | Stabilize manifold air at 0.55–0.60 MPa; replace worn Yamaha CL feeder pawl |
| False vision rejection on shiny QFN/SOP leads | Specular LED glare saturating the upward CCD sensor | Inspect live grayscale threshold mask during test pick | Reduce ring LED brightness by 20–30% and raise camera exposure gain |
| Skewed placement or tombstoning after reflow | Uneven solder paste release or excessive placement Z-force | Inspect post-placement paste impression under magnification | Reduce placement Z-depth by 0.08 mm; verify stencil aperture alignment |
| Placement bounce on thin (0.6–0.8 mm) PCBs | Unsupported board center flexing across the 3-stage rail | Observe center PCB deflection during Head 1–4 placement | Install magnetic center-support pins beneath the placement zone |
| 90° or 180° rotation offset on first article | CAD centroid zero-orientation mismatch (KiCad/Altium) | Overlay imported CSV rotation angles against reel orientation | Apply standardized rotation offset rules in the offline BOM mapping table |
Stabilizing Thin PCBs and Inline Conveyor Transfers
Placement accuracy depends just as heavily on board flatness beneath the gantry as it does on feeder indexing.
Supporting Multi-Up Panels Across the Three-Stage Rail
Thin FR-4 substrates (0.6 mm to 0.8 mm) and multi-up breakaway panels naturally bow downward across the center span of the CHM-551’s three-stage automatic conveyor. When a placement head drives a fine-pitch IC onto a flexing substrate, the board rebounds like a spring and knocks adjacent passives out of alignment.
Positioning magnetic support pins directly under non-populated zones of the bottom PCB surface restores rigid coplanarity, supporting contamination control reports and ISO cleanroom manufacturing quality targets for high-density electronics.
Shift-Start Preventive Maintenance Checklist
Running a five-minute verification sequence before starting each production batch prevents mid-run drift and unplanned line stops:
- Check Manifold Air Pressure: Confirm the inline gauge reads steady between 0.55 MPa and 0.60 MPa with zero moisture in the filter bowl.
- Wipe Optical Lenses: Clean both the upward-looking component camera and downward-looking mark camera with lint-free optical wipes and isopropyl alcohol.
- Test Nozzle Vacuum Seals: Run an automated nozzle check across all four spindles to verify clean pickup and drop-off response.
- Inspect Cover-Tape Tension: Confirm peeled carrier film tracks smoothly onto every feeder take-up spool without slack.
- Run a Dry Fiducial Check: Verify that the gantry locates global PCB fiducial marks within 0.02 mm before enabling component placement.
Consistent shift-start verification pairs directly with technical engineering checklists to maintain repeatable placement yields across multi-batch schedules.
Conclusion
Eliminating component mispicks and feeder drift on the CHM-551 depends on controlling four physical variables: regulated pneumatic supply pressure, optically taught feeder pick centers, calibrated Z-axis touchdown travel, and glare-free upward vision thresholds.
Treating shift-start nozzle checks, rail support pin placement, and periodic feeder pawl inspections as standard operating discipline keeps placement repeatability locked within its ±0.06 mm (CPK ≥ 1.0) specification across prototype and mid-volume production runs.
For facility-specific SMT line integration guidance, cleanroom metrology documentation, and equipment configuration support, explore Applied Physics USA or consult our application engineering team to optimize your assembly workflow.
CHM-551 Setup and Calibration Walkthrough demonstrates step-by-step feeder mounting, nozzle configuration, and vision calibration procedures directly on the CHM-551 platform.
Frequently Asked Questions (FAQs)
1. What causes component mispicks on the CHM-551 pick-and-place machine?
Component mispicks on the CHM-551 commonly result from restricted nozzle vacuum, incorrect feeder indexing, pneumatic pressure fluctuations, worn feeder pawls, or improper Z-axis pickup height. These issues prevent components from aligning correctly beneath the nozzle during high-speed placement cycles.
2. What is the recommended air pressure for Yamaha CL feeders on the CHM-551?
Yamaha CL pneumatic feeders generally require stable compressed air within the 0.5–0.7 MPa range. The article recommends maintaining approximately 0.55–0.60 MPa at the CHM-551 manifold to support consistent feeder indexing during simultaneous four-head operation.
3. Why does the CHM-551 sometimes pick up empty components or miss parts?
Empty-pick errors can occur when the feeder advances the carrier tape incorrectly, the nozzle bore becomes clogged, or the vacuum seal is insufficient. Incorrect tape pitch settings and loose cover-tape tension can also prevent components from reaching the correct pickup position.
4. How do you correct feeder drift on the CHM-551?
Start by checking that each feeder is fully seated and locked into its mounting rail. Verify pneumatic pressure, inspect ratchet pawls for wear, and check tape advancement under the downward-looking camera. Run multiple manual feed cycles to confirm that components remain centered beneath the pickup coordinates.