Surface Mount Technology (SMT) production lines depend on continuous, uninterrupted workflow.
When high-speed pick-and-place systems and automated stencil printers run at full capacity, even a momentary stoppage creates immediate line starvation.
Among front-end line equipment, the automatic PCB magazine rack loader plays a decisive role. It indexes magazines, extracts raw or pre-assembled printed circuit boards, and transfers them onto downstream conveyor tracks.
Despite being a mature piece of automation, the loader remains one of the most common sources of mechanical line stoppages.
Board jams, double-feeds, and cracked substrates not only stall production but also damage expensive circuit boards.
Eliminating these feeder errors requires understanding why jams occur and applying structured mechanical, sensor, and control fixes.
What Causes Board Jams in SMT Magazine Loaders?
Board jams rarely happen at random. They stem from mechanical wear, dimensional mismatch between boards and rack slots, uncalibrated pneumatic pushers, or sensor blind spots.
1) Substrate Warpage and Thin-Board Sagging
Modern electronics require thinner boards, ranging from $0.4\text{ mm}$ to $0.8\text{ mm}$, as well as flexible and rigid-flex designs. Thin substrates tend to sag across wider magazine spans. If a PCB has experienced pre-reflow warpage or thermal stress, its leading edge drops below the exit slot level.
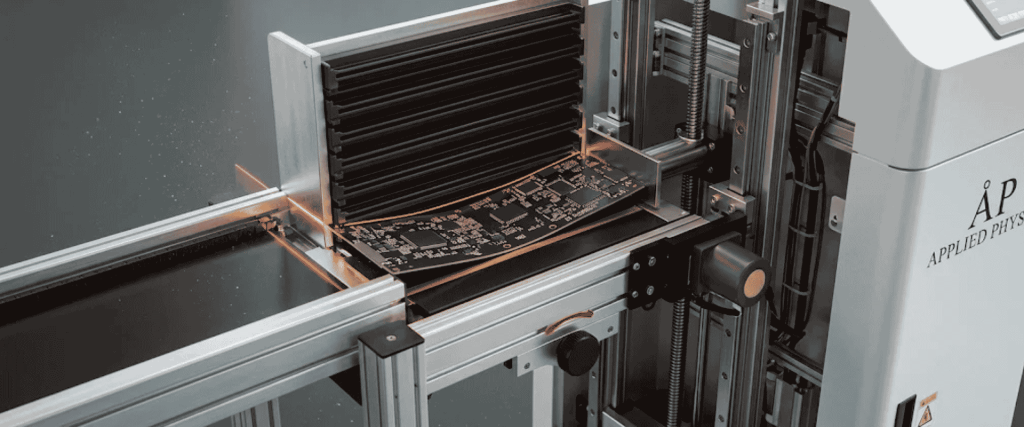
When the pusher blade advances, the substrate catches against the slot edge of the magazine rack, bending the panel or triggering a thrust fault.
2) Uncontrolled Pusher Blade Dynamics
Older or entry-level magazine loaders rely on basic pneumatic cylinders to drive the pusher knife. Pneumatic cylinders can deliver inconsistent, jerky thrust when line air pressure fluctuates.
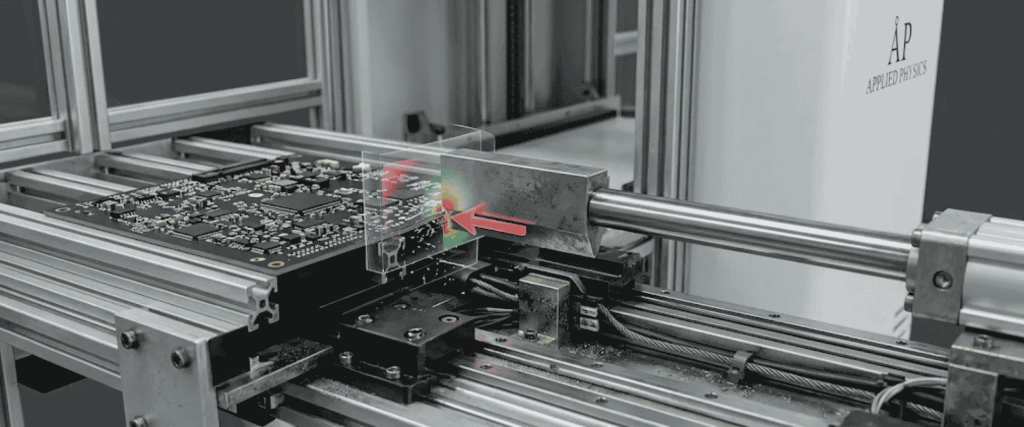
When a board meets minor resistance, a standard pneumatic cylinder continues pushing until full stroke, which can scratch bottom-side copper traces, scrape off solder mask layers, or fracture edge-mounted MLCC capacitors.
3) Elevator Indexing and Pitch Drift
The elevator mechanism shifts the loaded magazine rack vertically to align each board slot with the discharge conveyor. When lead screws wear out, stepper motors lose steps, or drive belts lose tension, the elevator drifts by even $0.5\text{ mm}$ to $1.0\text{ mm}$.
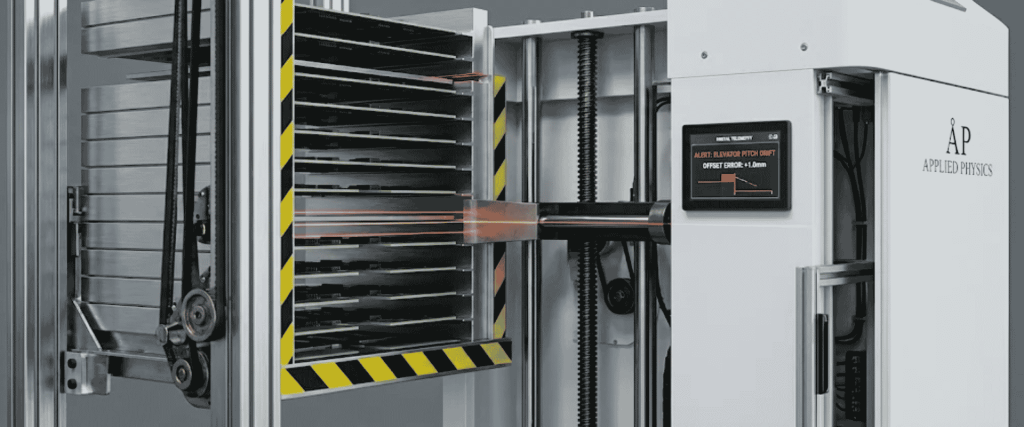
This minor deviation misaligns the pusher blade with the rack slot, forcing the pusher knife directly into the magazine frame rather than contacting the board edge.
4) Magazine Rack Deformation and Wear
SMT magazine racks endure heavy handling, repeated heating cycles during baking, and rough transport across shop floors.
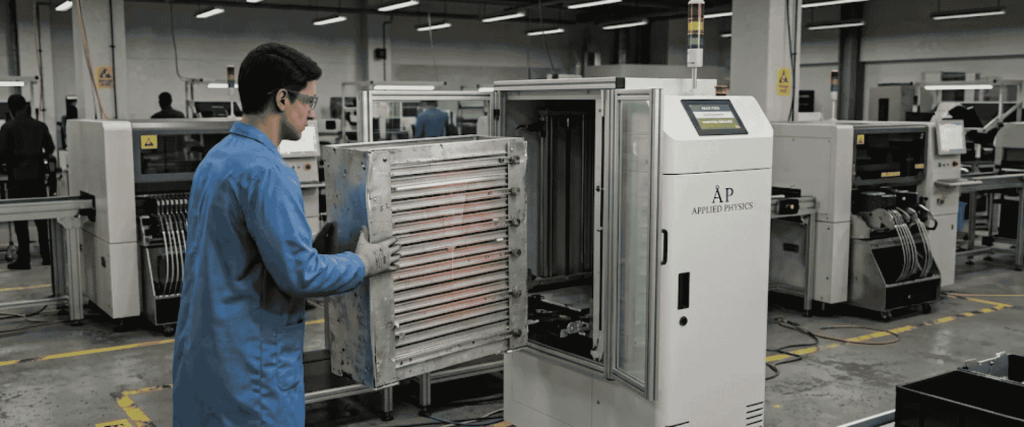
Warped aluminum side panels, loose thumb screws, and uneven slot spacing throw off the rack’s internal parallelism. If the front and rear track widths differ by even a millimeter, boards bind inside the channels during extraction.
5) Sensor Misreads and False Signals
Standard optical and through-beam sensors verify board readiness and line clearance. Dark solder masks (matte black, deep blue), open routing slots, board cutouts, and semi-transparent ceramic substrates reflect light unpredictably.
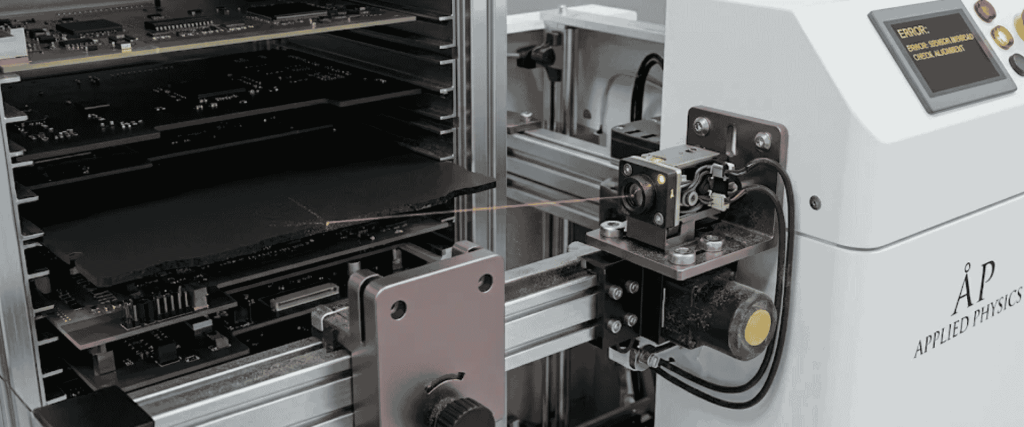
When a sensor fails to register a dark board, the loader attempts a second push or skips an index pitch, causing a direct collision.
Core Causes and Engineering Solutions for Board Jams
| Root Cause | Immediate Operational Impact | Engineering Solution | Preventative Action |
| Pneumatic Pressure Spikes | Inconsistent stroke speed; board edge crushing | Replace with motor-driven, torque-limiting pusher systems | Install secondary pneumatic regulators and lubricators |
| Elevator Pitch Misalignment | Pusher knife hits rack divider; double feeding | Recalibrate motor step counts via PLC touch panel | Inspect ball screws and tension stepper drive belts monthly |
| Magazine Rack Tapering | PCBs bind inside slot before clearing rack | Use rigid gauge blocks to standardize rack width | Retire racks showing slot burrs or bent side panels |
| Thin Substrate Sag | Leading edge dips below track entry point | Install front-edge mechanical support guides | Lower push speed parameters for boards under $0.8\text{ mm}$ |
| Optical Reflection Failures | Pusher fires out of sequence or skips slots | Switch to diffuse laser sensors or background-suppression optics | Clean optical lenses weekly with lint-free alcohol wipes |
| ESD Grounding Gaps | Static cling causes boards to drag against slots | Check chassis ground pathways and ESD brush contacts | Monitor conductivity between rack clamps and ground rails |
Practical Steps to Prevent Loader Jams
Addressing board jams requires systematic changes across mechanical setup, pusher control, and line integration.
Switch from Uncontrolled Pneumatics to Motorized Pusher Control
Modern SMT operations favor loaders equipped with electric motor drives and precision ball screws over pure pneumatics. A programmable motorized pusher allows precise control over:
- Initial Acceleration: Starts slowly to cleanly release the PCB from the magazine friction points.
- Mid-Stroke Velocity: Moves the board swiftly across the transfer gap.
- Torque Limiting: Stops the stroke immediately if resistance exceeds a safe threshold, preventing cracked panels.
Standardize Magazine Rack Calibration Protocols
Never assume every magazine rack on the shop floor maintains identical dimensions. Implement regular rack maintenance:
- Parallelism Verification: Measure rack width at the front, middle, and rear using an internal vernier caliper or setting fixture.
- Locking Mechanism Inspections: Verify that rack clamping bars hold firm under elevator movement.
- Slot Integrity Checks: Remove racks with nicked, burred, or deformed guide slots from the production loop.
Optimize Sensor Sensitivity for Diverse Board Colors
Modern PCB designs feature complex surface coatings. To avoid false empty-slot or jam alarms:
- Use photoelectric sensors with adjustable focal ranges and background suppression, ensuring consistent detection regardless of whether the PCB surface is green, black, white, or bare copper.
- Adjust sensor positions so the beam strikes solid board material rather than panel routing slots, breakaway tabs, or edge holes.
Establish Secure Line Communication via SMEMA and IPC Standards
A magazine loader does not operate in isolation. It relies on standard handshakes with the downstream machine, typically an automatic stencil printer or an inspection conveyor.
- Ensure SMEMA (Surface Mount Equipment Manufacturers Association) hardware relays trigger cleanly without electrical noise.
- Where available, adopt digital protocols such as IPC-HERMES-9852 to pass exact panel dimensions, pitch steps, and magazine lane coordinates down the line before boards begin moving.
Conclusion
Board jams in SMT automatic magazine rack loaders remain a major, preventable cause of factory downtime.
While frequent stoppages are often dismissed as simple operator error or bad substrate lots, they typically point to mechanical misalignment, uneven rack widths, or unbuffered pusher forces.
By upgrading to motorized pusher drives with PLC torque control, instituting strict magazine rack dimensional checks, and tuning sensor arrays for diverse board finishes, manufacturing teams can eliminate front-end feeding bottlenecks.
These straightforward engineering practices protect sensitive board assemblies, stabilize line cycle times, and preserve overall production yield.
Frequently Asked Questions (FAQs)
1. How often should SMT magazine rack dimensions be checked?
Inspect and calibrate magazine rack width and channel parallelism monthly, or immediately if a rack is dropped or exhibits repeated extraction friction on the line.
2. Why does the loader pusher blade miss the magazine slot?
This issue typically results from elevator pitch drift caused by loose stepper drive belts, a worn vertical lead screw, or an incorrect pitch setting programmed in the PLC recipe.
3. Can automatic magazine loaders handle thin or flexible boards?
Yes, provided the loader uses thin-board support guides, slower initial pusher feed rates, and multi-point clamping to keep the panels flat as they transition onto the conveyor.